Chemical Etching
Etched Foil Heating Elements
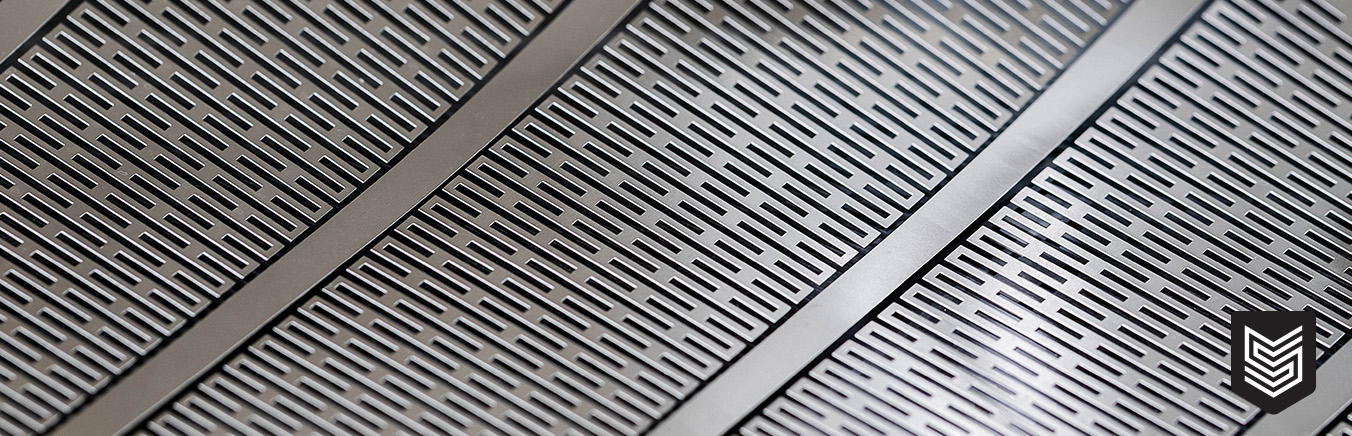
In industrial thermal operations, thermal lag is a widespread problem. In traditional heaters like cartridge heaters, tubular elements, and cast-in plates, the significant mass of the heaters and heavy mounting plates means that thermal inertia is present. As energy is wasted in heating heavy mounting structures, startup, temperature changes, and temperature overshoot are delayed, with the potential for damaging the materials. Thus, thermal lag can limit the efficiency of processes requiring rapid cycling or those that have strict limits on operation.
Etched foil heating elements eliminate this problem by reducing thermal mass. Bonding thin etched resistive circuits to insulating substrates places heat directly at the working surface. Energy passes directly to the process rather than being absorbed by the metal parts. This characteristic low thermal mass provides quick heating of the process, fast cooldown periods, and accurate thermal regulation.
Etched foil heaters operate with minimal internal heat storage. Because the resistive foil is thin—often just a few thousandths of an inch—it requires minimal energy to reach operating temperature.
Current flowing through the trace heats the foil in seconds. When current stops, heat dissipates almost instantly, delivering clear operational advantages:
Claims about energy efficiency require clear technical context. Low thermal mass does not create energy from less power; efficiency gains stem from operational velocity and targeted energy delivery. Less power is wasted heating heavy structural masses during startup, and cycle times decrease because equipment reaches setpoints faster.
An etched foil heating element is an engineered resistive circuit. Its thermal performance depends directly on electrical resistance. The electrical resistance $R$ of a conductive trace is defined by:
$$R = \frac{\rho L}{A}$$
where $\rho$ represents material resistivity, $L$ is trace length, and $A$ is cross-sectional area (trace width multiplied by foil thickness). Heat output or power $P$ relates to operating voltage $V$, current $I$, and resistance $R$ through standard power equations:
$$P = \frac{V^2}{R} = I^2 R$$
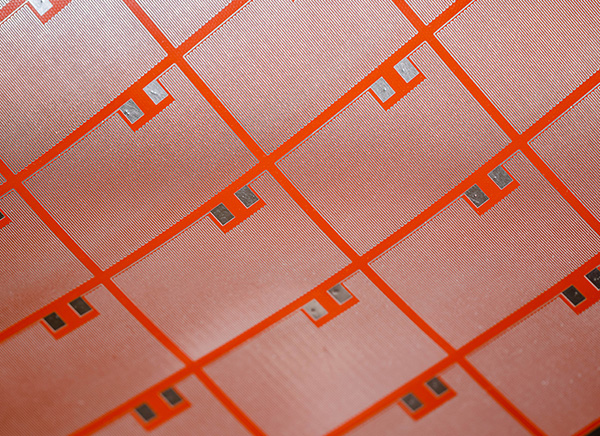
Controlling trace geometry is essential because watt density depends directly on resistance. Photochemical Machining (PCM) lets engineers adjust trace width, length, and routing across the heater face.
In many applications, heat escapes faster near outer edges than from the center, leaving cold spots. With etched foil, designers adjust circuit artwork to compensate. Traces can be made narrower near outer edges to increase local watt density, while wider trace spacing in the center reduces heat output where losses are low. This custom geometry produces uniform temperatures across the surface.
 Why Photochemical Machining Outperforms Mechanical Cutting
Producing long, intricate resistive traces in thin metal foil requires a manufacturing method that preserves metal integrity. Mechanical stamping, die cutting, or laser cutting can introduce physical defects along foil edges. Cutting tools pull and deform thin metal, leaving heavy burrs and internal mechanical stress. Laser cutting generates heat-affected zones that alter local metallurgy along the cut edge.
These defects alter local cross-sectional area $A$ along the trace. A minor reduction in trace width or thickness creates a localized resistance spike. This sharp increase causes a hotspot leading to the premature burning of the heating element.
Using chemical etchants, photochemical machining dissolves unnecessary metal without the use of force or heat. Because of this, it gets clean edges with no burrs and doesn’t induce any mechanical stress or heat.
Digital phototooling provides another major advantage. Switzer leverages PCM to make prototyping fast and cost-effective. If thermal testing requires higher resistance or modified heat distribution, engineers simply update the artwork file. Producing a new phototool takes days rather than weeks required to modify steel dies, allowing engineering teams to iterate quickly without hard tooling costs.
Dimensional inspection is standard in metal manufacturing, but precision heaters require a different quality focus. While checking trace width and foil thickness confirms physical shape, electrical resistance is the functional specification governing heater performance.
Raw foil thickness can vary slightly across a coil. A deviation of a few ten-thousandths of an inch shifts overall resistance across a long trace. That shift alters total wattage and thermal output under load.
Switzer approaches manufacturing from a functional perspective. PCM allows electrical performance to be engineered directly into foil geometry. Instead of evaluating parts strictly against dimensional tolerances, Switzer inspects heater circuits based on resistance in ohms. Testing against functional electrical output confirms that every lot delivers predictable thermal performance in the field.
Etched foil heaters are particularly suitable for applications where there are spatial restrictions as well as the need for uniform heat distribution and quick heat-up:
Improving process efficiency comes down to delivering thermal energy without delay. Photochemical machining allows engineers to turn complex circuit designs into precise foil heaters that eliminate thermal lag and shorten cycle times. Partnering with Switzer streamlines the transition from initial design concepts to high-volume production, creating reliable thermal solutions built for long-term operational success.
4020 Jeffrey Blvd. | BUFFALO, NY 14219
P: (716) 821-9393 / (800) 875-1093
Website by Luminus