Chemical Etching
Metal Fabrication
A small supplier can be essential to a large aerospace or defense program. It may produce a thin metal screen or a precisely etched aperture that few general fabricators want to take on. The prime contractor still has to manage the risk of placing that part with a smaller company. Can the supplier repeat the result after the prototype? Will the records show what material went into each lot? What happens when the drawing changes?
Those questions deserve evidence from the shop floor. Supplier size gives a buyer little insight into process control, and a good sample alone cannot establish production readiness. A specialty manufacturer earns its place by showing how it will make and deliver the approved part throughout the program.
A sound quality system should be visible in ordinary work. Ask how the shop links a delivered part to the incoming material lot and the approved drawing revision. Follow that record through production and inspection. Calibration records should show that the measuring equipment was fit for use when the lot was accepted.
Then ask to see what happens to a nonconforming part. It needs to be identified and controlled so it cannot reenter accepted stock without the proper disposition. Corrective action should address the cause, with evidence that the fix worked. Supplier controls and record retention matter when material or secondary finishing comes from another source.
Switzer regularly hosts customers for site visit and quality/full process audits. A useful audit follows a real component through manufacturing and documentation. It gives the program team a chance to assess controls firsthand, including how people respond when a result falls outside the approved plan.
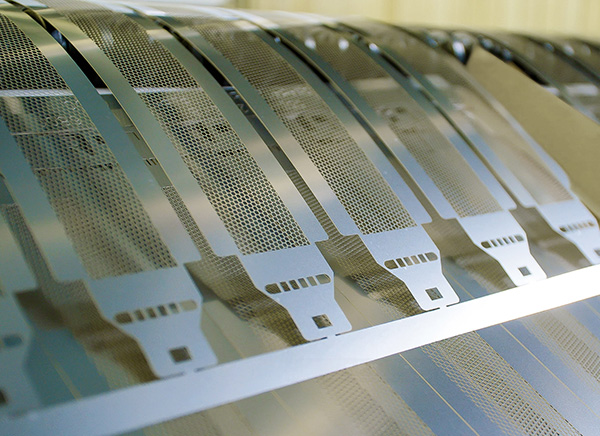
For an etched screen, compare the material lot and phototool revision on the traveler with the finished lot record. Check the inspection criteria and the disposition of rejected sheets. This tests whether written controls work on the floor.
 Prove Repeatability
Photochemical machining (PCM) can make complex features in thin metal without a hard stamping die. That flexibility helps when a drawing changes during development. It does not excuse loose control after the design is approved. The supplier must manage phototool versions, imaging, etch conditions, and inspection so the next lot agrees with the qualified part.
A first article gives the customer a documented starting point. Production evidence matters after that. Review how the manufacturer checks critical dimensions across lots and responds to process drift. The material thickness, web width, and any later forming step can affect repeatability. A supplier that understands its process window should be able to explain which measurements are most sensitive and how it keeps them under control.
A quiet material substitution can have consequences even when a new sample looks right. The same is true of a new finishing source or revised phototool. Aerospace customers need an agreed change process that records what changed, why it changed, and which approvals are required before affected parts ship.
Revision control begins with the drawing but extends to work instructions and inspection plans. If a change affects fit or performance, the customer may require another first article or further qualification. Ask the supplier how it segregates old and new inventory during the transition. Traceability is useful only when it can connect a delivered lot to the exact approved configuration.
Switzer’s PCM capabilities suit thin metal parts with fine geometry. Aerospace programs may need shims, screens, filters, EMI/RFI components, apertures, or spacers. A design review can reveal whether etching is a sensible process for the specified material and features, or whether a secondary operation needs attention before the design is frozen.
There is a practical advantage in speaking directly with engineering and quality staff at a focused supplier. A drawing question can reach the people who understand etch behavior and inspection. Production and leadership can join when a material problem threatens the schedule. Direct access does not replace the prime’s approval process. It can help the teams identify a workable response quickly and document it properly.
For a revised aperture, the supplier should explain the effect on etching and inspection. The customer’s engineer checks the effect on the assembly before approving a new version.
A qualified component cannot support a program if it arrives after the assembly slot. Ask about material availability, capacity, and the forecast the supplier needs. Packaging should protect fine features during shipment. Review delivery history and discuss demand changes early.
Switzer’s production approach includes inventory planning and scheduled releases. Customers can discuss production against forecast demand and holding approved parts for later release. That arrangement needs agreed quantities and clear revision control, especially when a design change leaves older stock on the shelf.
Identify held stock by revision before shipping it after a change.
A small specialist can support a large program when it makes its process visible. The prime needs proof of repeatability, a clean record of changes, access to the technical team, and a supply plan it can trust. Those are concrete questions to put on the table before an award, and they remain useful long after the first part ships.
4020 Jeffrey Blvd. | BUFFALO, NY 14219
P: (716) 821-9393 / (800) 875-1093
Website by Luminus